Knowing exactly how to read a calibration certificate is an indispensable skill for quality assurance managers, metrologists, and compliance officers. In this article, we will break down how to read a calibration certificate in 5 easy steps to ensure your facility remains audit-ready.
Knowing exactly how to read a calibration certificate is an indispensable skill for quality assurance managers, metrologists, and compliance officers.
This ultimate guide breaks down every advanced metric, standard, and technical line item on an accredited certificate to ensure your facility remains audit-ready and operating at peak accuracy.
A calibration certificate is a legally binding, technical statement of an instrument’s performance at a specific point in time. Simply checking for a Pass or Fail stamp is a major compliance risk during strict audits.
Modern global quality systems—including ISO 9001, IATF 16949, and FDA 21 CFR Part 11—demand rigorous verification of calibration data. Every instrument utilized in production must be linked directly to an internationally recognized standard.
This core requirement is managed globally through strict ISO/IEC 17025 Accreditation, which validates that the laboratory itself possesses the technical competence and equipment necessary to deliver trustworthy data.
While layouts vary between laboratories, accredited calibration facilities structure their documents according to international metrology standards. The document is divided into administrative metadata and empirical measurement data.
Administrative Metadata and Traceability
The top section establishes the administrative tracking of the asset:
Metrological properties shift based on physics. The document records precise ambient parameters during testing:
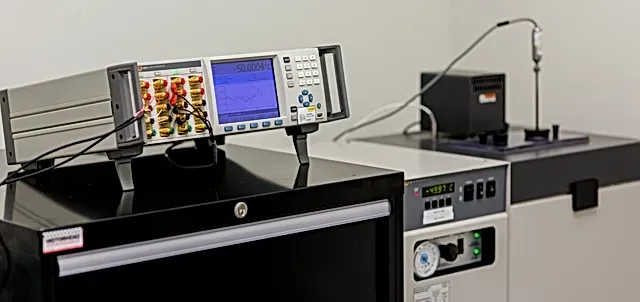
The core value of the document lies within the empirical test results. Interpreting these metrics correctly prevents catastrophic production deviations.
Nominal Value vs. Reference Actual Value
As-Found vs. As-Left Data Matrix
This is the most critical historical data stream for quality managers:
The deviation represents the inherent systematic error of your asset. The standard formula is: Deviation equals Instrument Reading minus Reference Actual Value.
A positive deviation means your device reads higher than the true value. A negative deviation means it reads lower.
No physical measurement can be perfectly precise. Every measurement carries an inherent envelope of doubt, formally known as Measurement Uncertainty.
Accredited laboratories calculate this according to the ISO Guide to the Expression of Uncertainty in Measurement. On your certificate, this is presented as Expanded Uncertainty, calculated using a coverage factor of k=2, which represents a 95 percent confidence interval.
This means that if your instrument reads 50.00 mm with an uncertainty of plus or minus 0.02 mm, there is a 95 percent statistical probability that the true, absolute value falls anywhere between 49.98 mm and 50.02 mm.
When configuring complex machinery or dealing with heavy machinery tolerances, leveraging dedicated Industrial Calibration Solutions ensures that your uncertainty budgets remain tightly controlled and well below your process limitations.
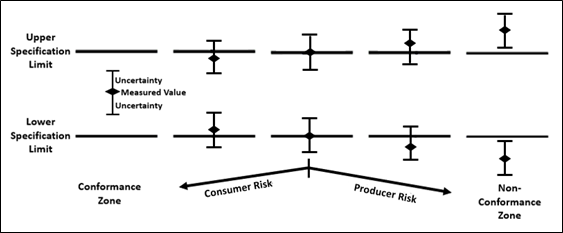
How do laboratories determine if an instrument officially passes or fails? They apply a Decision Rule. Under advanced standards like ILAC-G8, laboratories utilize Guard Banding to manage the risk of false acceptance.
A critical metric for high-stakes manufacturing is the Test Uncertainty Ratio. It compares the tolerance of your device to the uncertainty of the calibration process. The standard formula is: Test Uncertainty Ratio equals Tolerance of Device Under Test divided by Expanded Measurement Uncertainty.
An industry standard ratio of 4 to 1 or higher ensures that the calibration process is at least four times more precise than the instrument being tested, minimizing consumer risk. For highly sensitive systems, sourcing specialized Calibration Services guarantees that the laboratory’s master standards meet these high-ratio prerequisites.
Receiving your paperwork back from the lab is only half the battle. To satisfy international auditors, implement this formal post-calibration workflow:
When dealing with multi-parameter devices such as digital multimeters, process calibrators, or environmental chambers, learning how to read a calibration certificate becomes slightly more complex. These advanced documents do not just present a single data table; they contain multi-layered matrices that require systematic analysis.
If you want to know how to read a calibration certificate for a multi-function asset, you must first look at the function sub-headings. For instance, a fluke calibrator certificate will have separate sections for DC Voltage, AC Voltage, Resistance, and Frequency. Quality compliance officers often make the mistake of checking only the first page. However, understanding how to read a calibration certificate thoroughly means verifying every single function sub-table against your internal process tolerances to ensure no hidden out-of-specification drift exists on secondary functions.
Statistical data shows that many laboratory clients fail their ISO audits simply because they do not fully understand how to read a calibration certificate correctly. Avoiding these standard operational pitfalls will keep your quality management system bulletproof:
Training your internal calibration technicians on how to read a calibration certificate prevents these human errors. When a quality auditor asks your team to justify an instrument’s reliability, your staff must be able to demonstrate exactly how to read a calibration certificate and point directly to the metrological traceability statement and the expanded uncertainty parameters.
As Industry 4.0 integrates into modern manufacturing, the traditional methods of how to read a calibration certificate are shifting from paper files to Digital Calibration Certificates (DCC). A DCC utilizes XML or JSON formats to allow automated quality control systems to read, interpret, and archive data without manual human intervention.
However, until your facility fully transitions to automated cloud systems, knowing how to read a calibration certificate in PDF or paper format remains a foundational requirement for daily risk management. Whether you are analyzing a mechanical pressure gauge document or a high-tech biomedical analyzer report, mastering how to read a calibration certificate ensures that your production lines run with absolute mathematical certainty.
Mastering how to read a calibration certificate transitions your quality team from passive paper-filers to proactive risk managers. By understanding how systematic error interacts with measurement uncertainty and enforcing strict decision rules, you safeguard your brand from costly product recalls and engineering failures.
Do you have instruments that require high-ratio, fully traceable testing? Reach out to our metrology engineers directly through our official Contact Page to schedule an accredited calibration run tailored to your operational specifications.
Implementing a rigorous verification workflow is the final step in securing your facility’s data integrity. Quality engineers must ensure that every single interpreted metric is logged systematically to observe long-term asset drift. Over time, analyzing these micro-shifts allows your technical team to optimize calibration intervals safely, reducing operational costs while staying strictly compliant with global standards. For continuous engineering insights, sector-specific case studies, and updates on global metrology standards, make sure to follow our official Calibration Blog.
If your internal audit cycle is approaching and you need to verify the precision of your multi-brand equipment inventory, selecting a highly capable laboratory partner is paramount. You can explore our full range of accredited parameters and specialized on-site solutions directly through our ISO/IEC 17025 Calibration Services page. For immediate technical assistance, custom price quotes, or to schedule an upcoming equipment optimization run, please reach out to our engineering support team through our dedicated Contact Page.